Manufacturing & Delivery Case · Salamanca, Spain

Curved materials, controlled as one package.

Seven decorative product families translated from renderings and CAD into 72 trial-fitted assemblies, completed for shipment in 26 days.

72Assemblies
7Product families
26Calendar days
01 / The brief

A procurement company required one-to-one visual fidelity across curved glass, PVD stainless steel, water-ripple metal and concealed warm lighting.

LocationSalamanca, Spain
Completed for shipmentAugust 2023
Client typeProcurement company
Design inputRenderings, CAD, dimensions
Primary material304 stainless steel
InstallationClient team + remote guidance
02 / Scope

One coordinated package

Seven product families.
Seventy-two assemblies.

Different geometries, finishes and mixed-material interfaces were controlled under one engineering, trial-fit and delivery workflow.

12

Illuminated feature screens

304 stainless steel, glass, rose-gold PVD, anti-fingerprint treatment and lighting.

10

Curved glass partitions

Rose-gold PVD frames, warm light and 5 mm textured tempered glass.

9

Illuminated mesh pendants

PVD stainless-steel framework with concealed lighting.

18

Semicircular booth partitions

Rose-gold stainless steel, textured glass and warm LEDs.

2

Curved mesh booth features

304 stainless frame and mesh with warm lighting.

8

Water-ripple ceiling features

Mirror-finished water-ripple stainless steel and lighting.

13

Circular wall features

Natural stainless steel with CD texture and warm backlighting.

The critical item

Making rigid metal follow curved glass.

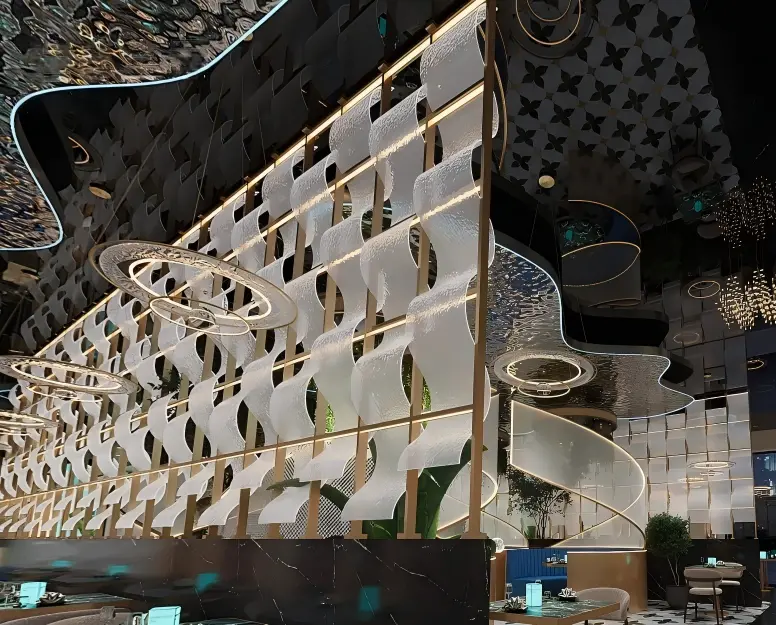
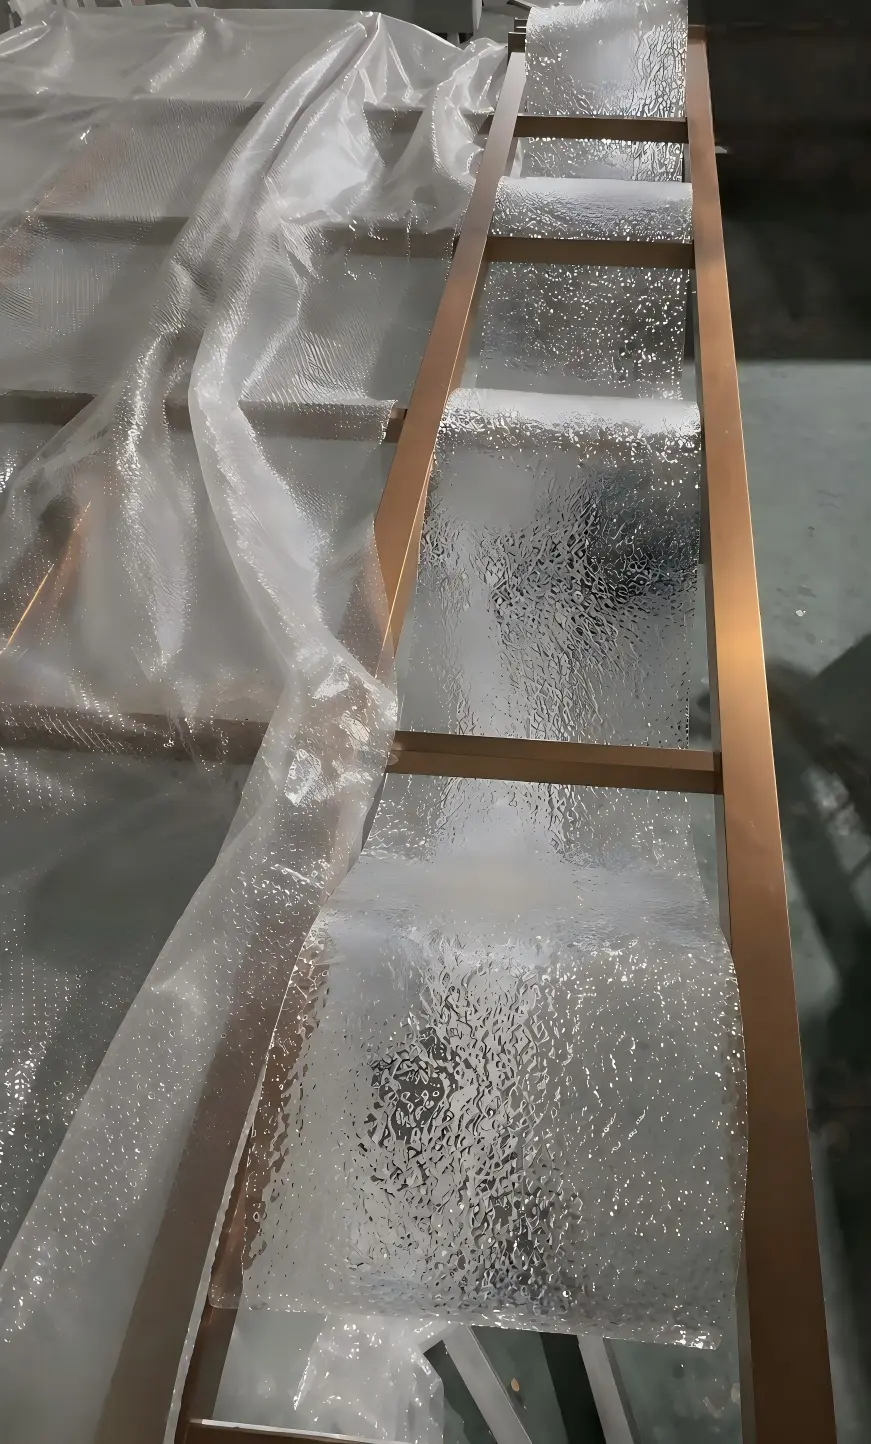
The 5 mm textured tempered glass changed continuously across a 2.5-metre-wide curve. Horizontal stainless members had to sit directly against that surface while preserving alignment and finish quality.
2.5 mUnit width
2.2 mUnit height
5 mmGlass
Physical fittingCurved interfaces were proven against the actual glass before series production.
Concealed wiringElectrical routes were hidden inside the stainless-steel tubes.
Modular deliveryUnits were separated for shipment and prepared for site assembly.
Client design inputRendering of a curved textured-glass partition
Factory completedCurved textured-glass partition assembled in the factory
Design targetClient rendering of the curved partition
Physical fitFactory-completed curved glass partition
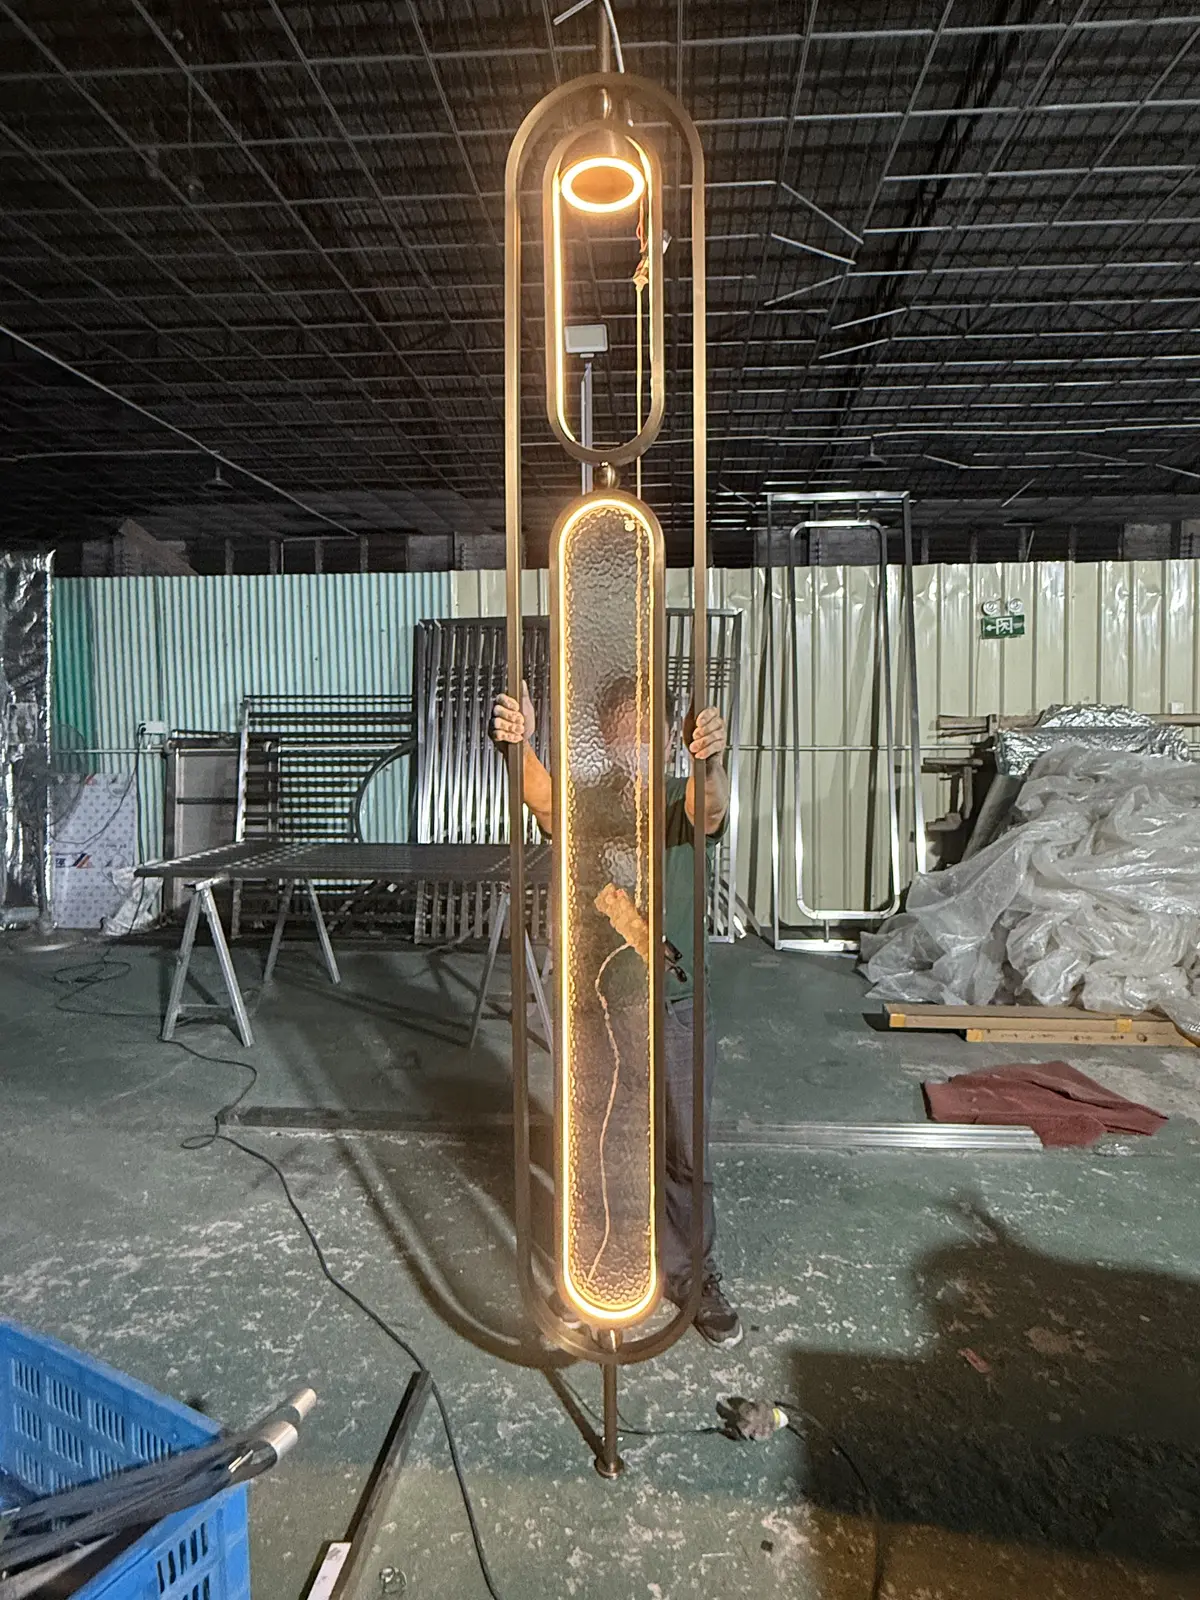
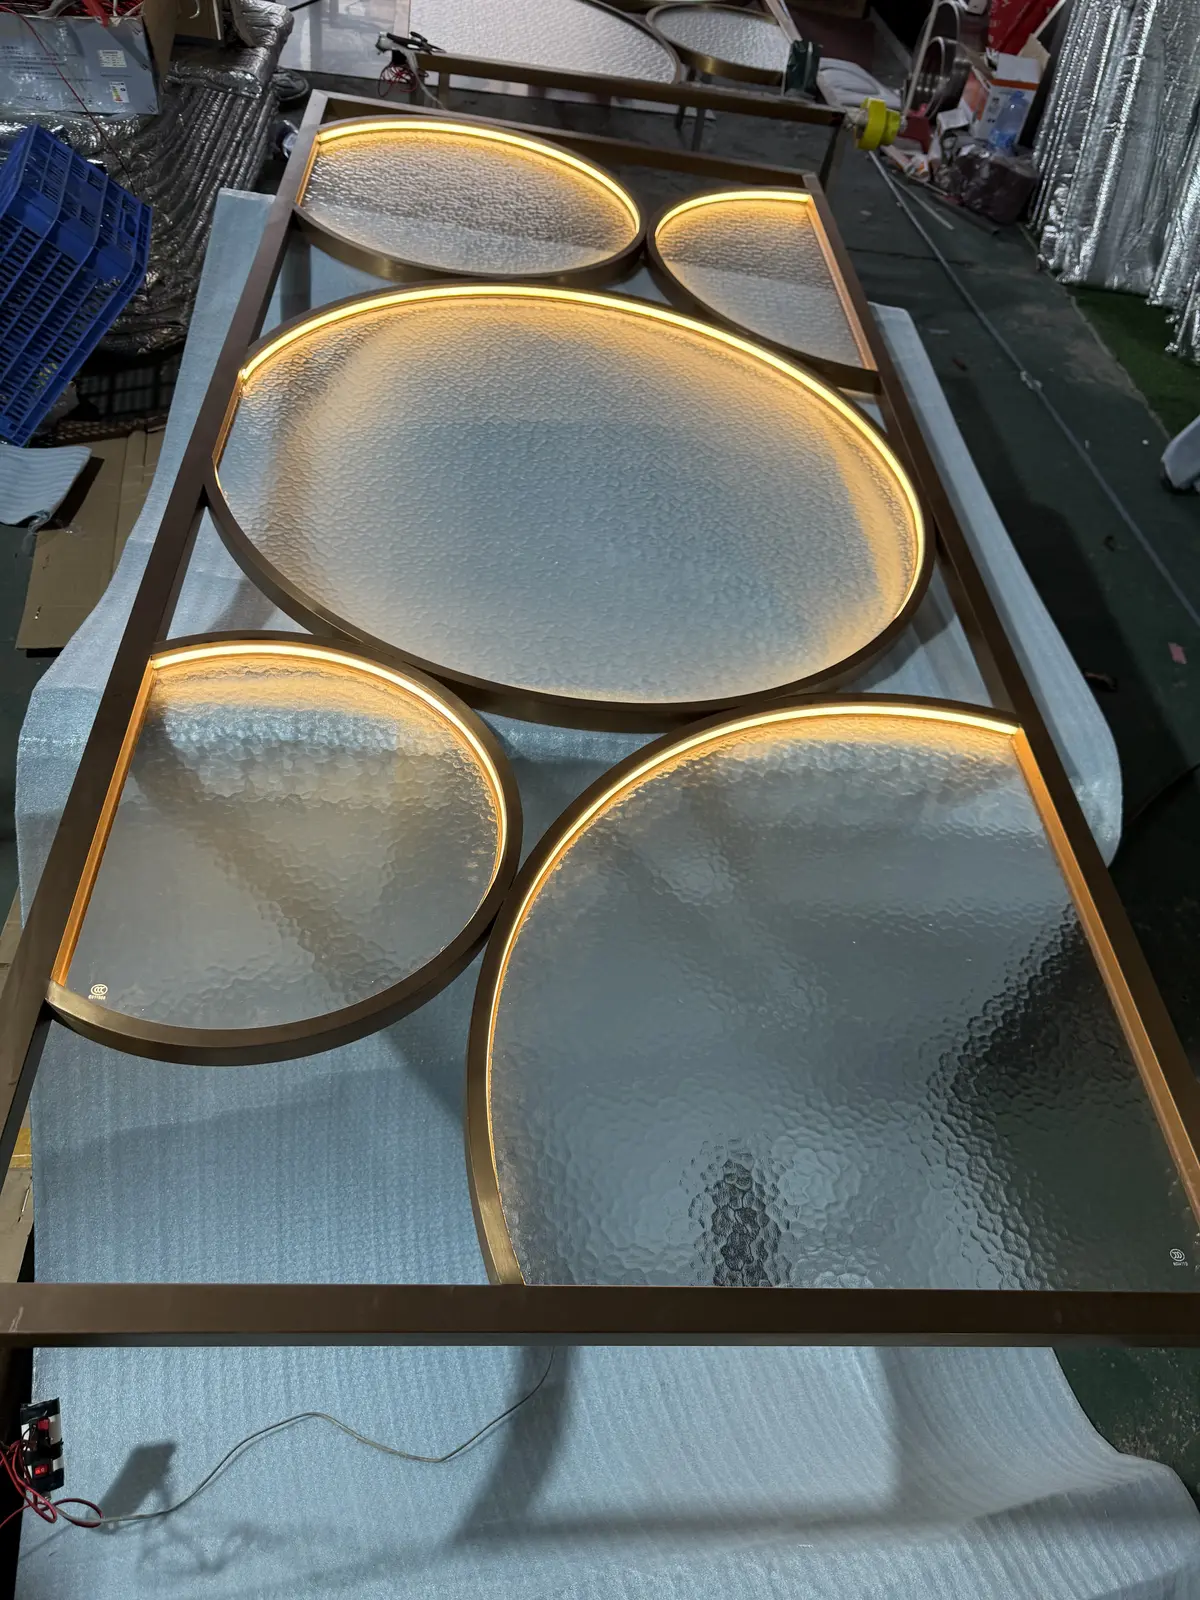
Illuminated screenCompleted illuminated feature screen
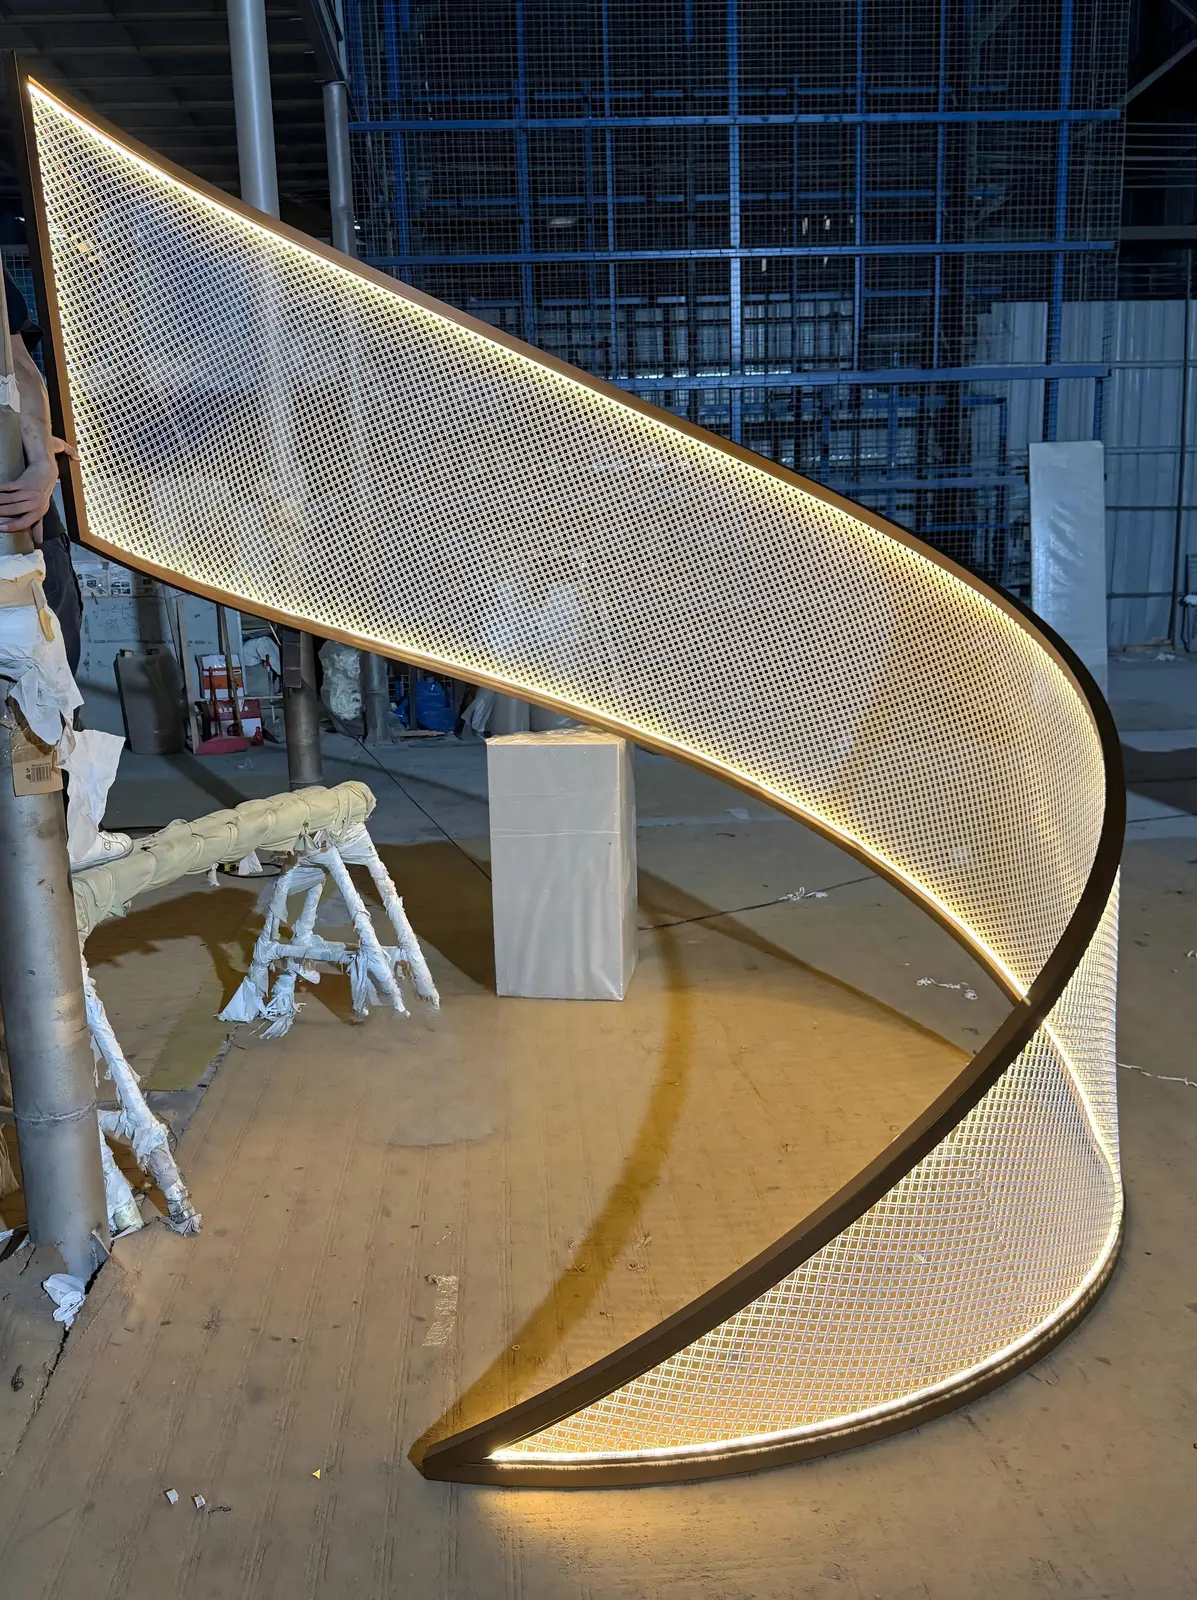
Mesh featureCurved stainless-steel mesh feature in the workshop

Manufacturing response

The first assembly did not fit. It was remade.

The first curved-glass unit could not be combined correctly. Instead of forcing the parts together, the glass-to-metal relationship was re-established through physical fitting and a replacement was produced.

  1. 01Compare the actual glass with the intended CAD geometry
  2. 02Locate interference across the changing radius
  3. 03Rework metal geometry against the physical glass
  4. 04Rebuild and verify the second assembly successfully
  5. 05Apply the corrected method to the remaining units
2Build iterations
to prove the interface

A controlled correction

One failed fit became a repeatable method.

The revised unit established the real relationship between curved glass and steel before series production continued.

One-to-one visual intentThe rendering remained the benchmark throughout the correction.
No dispatch delayThe package still shipped within the agreed 26-day period.
03 / Product range

Renderings to factory records

Multiple finishes, one visual language.

Selected pairs connect design intent with the physical assemblies produced in the workshop.

Illuminated feature screens

Glass, rose-gold PVD and warm light.

Twelve screens combine 304 stainless steel, glass, integrated lighting, rose-gold vacuum PVD and anti-fingerprint protection.
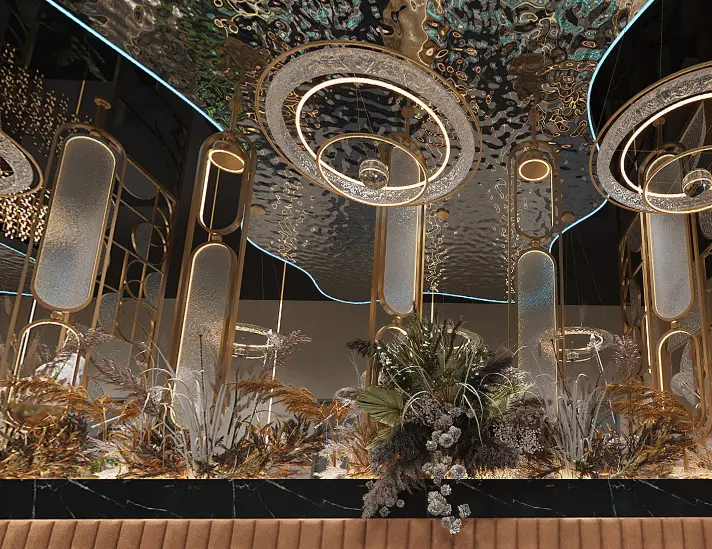
Client renderingRendering of an illuminated feature screen
Factory completedCompleted illuminated feature screen

Semicircular booth partitions

Repeated geometry across eighteen units.

Rose-gold PVD frames, textured glass and warm lighting were integrated into a repeatable curved format.
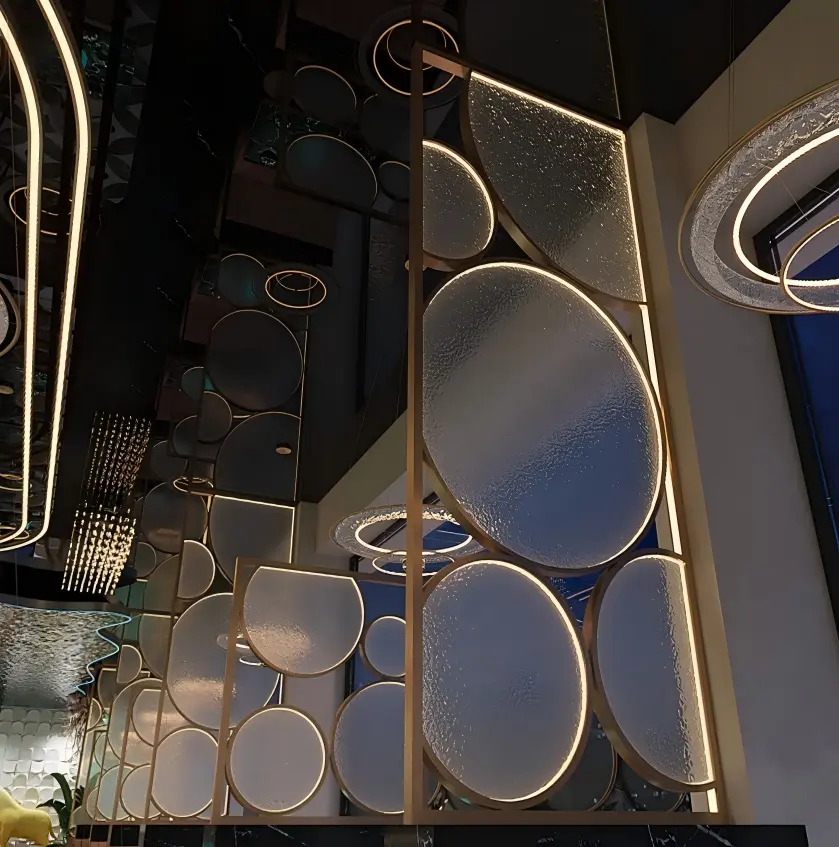
Client renderingRendering of a semicircular booth partition
Factory completedCompleted semicircular booth partition

Water-ripple ceiling features

Pressed texture, mirror finish, controlled light.

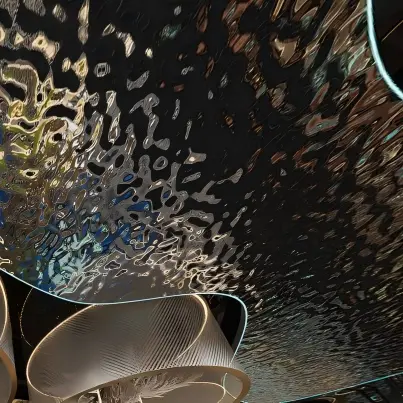
Eight ceiling features used water-ripple stainless steel with integrated warm lighting.
Design referenceRendering of a water-ripple ceiling feature
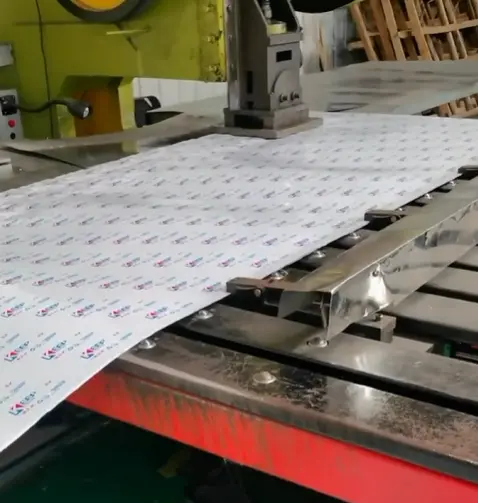
Forming processWater-ripple stainless steel during forming
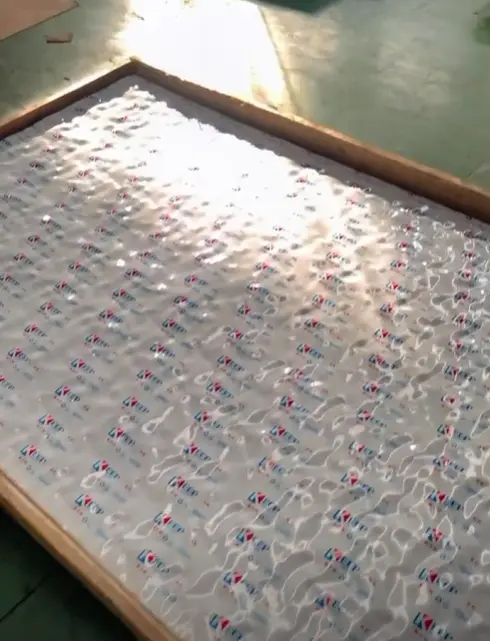
Finished surfaceFinished water-ripple mirror stainless steel

Circular wall features

Thirteen CD-pattern stainless forms.

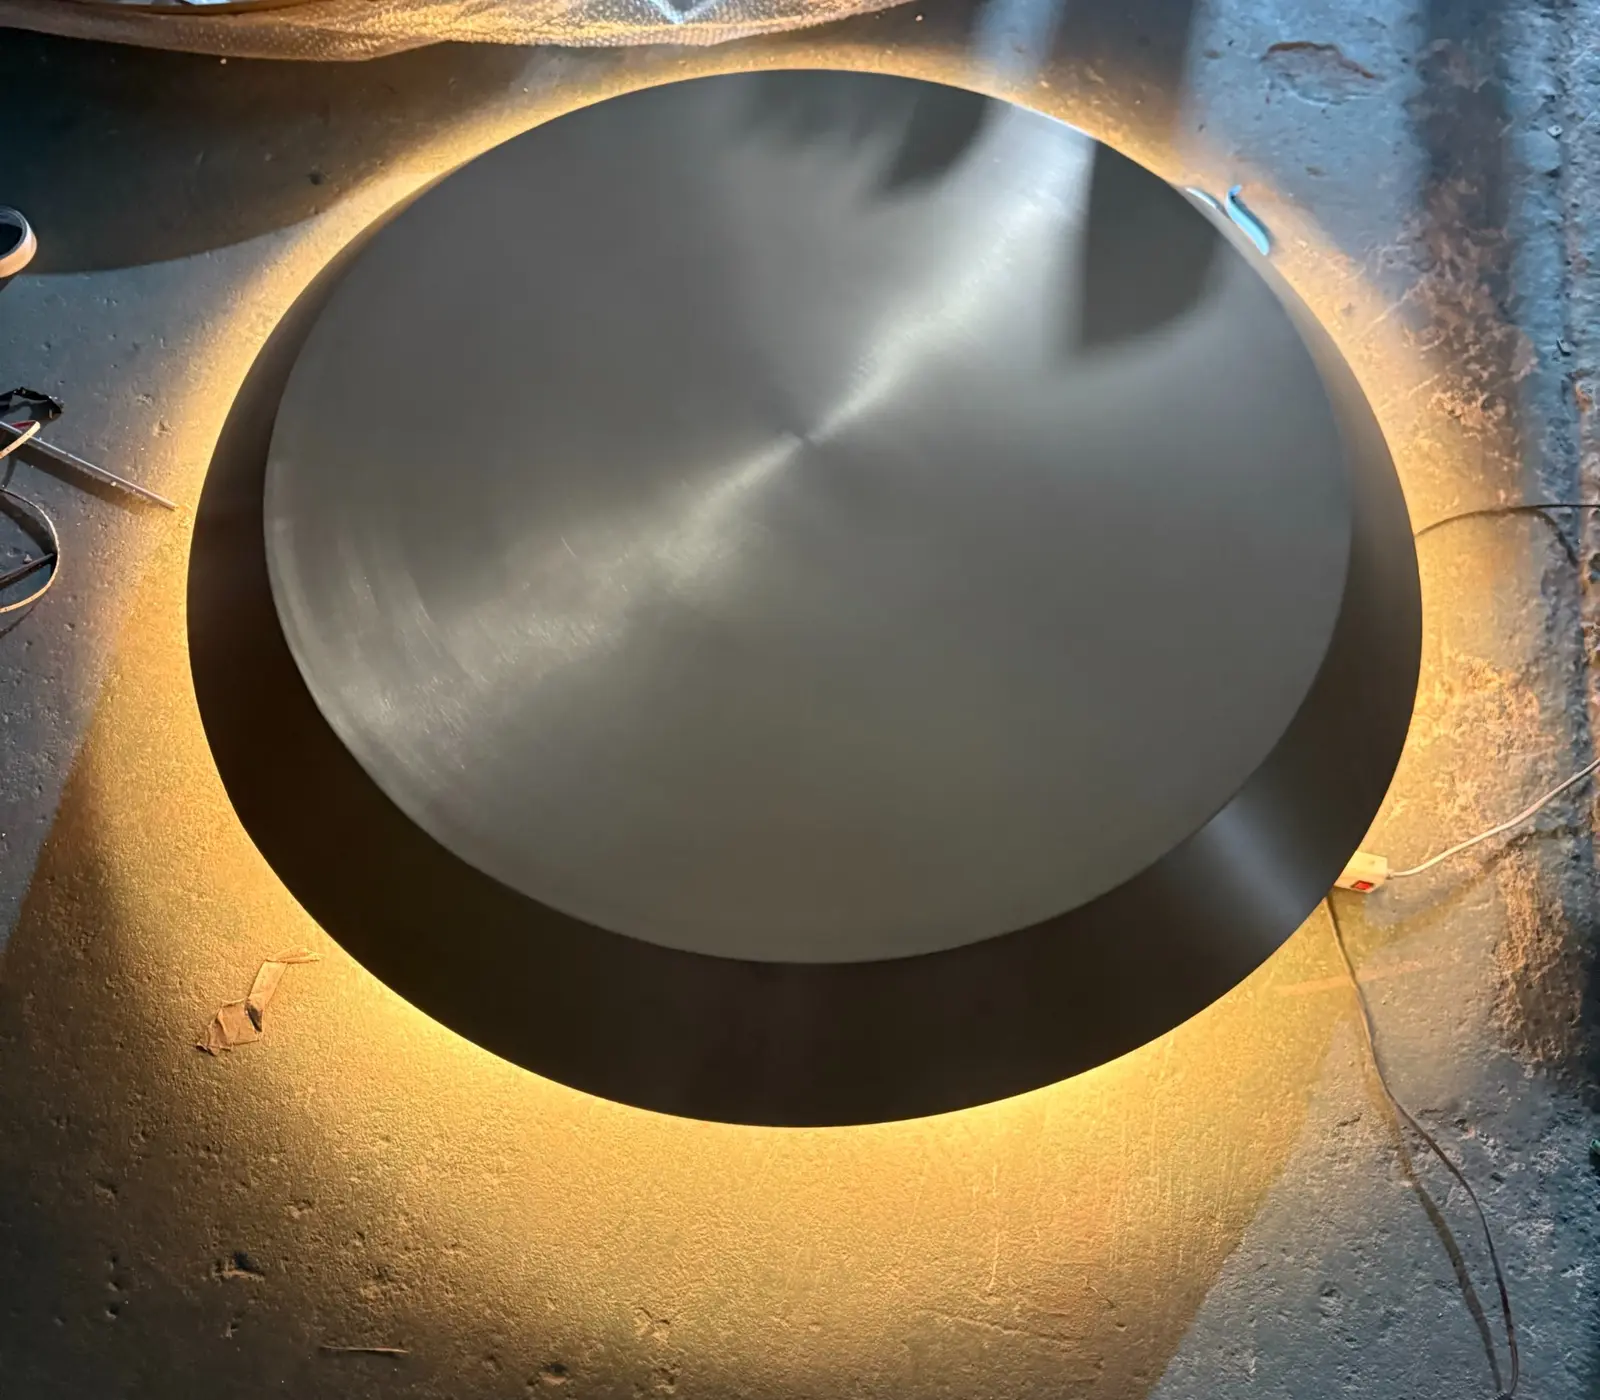
Natural stainless steel, CD-pattern treatment and warm backlighting were coordinated as a consistent wall-mounted family.
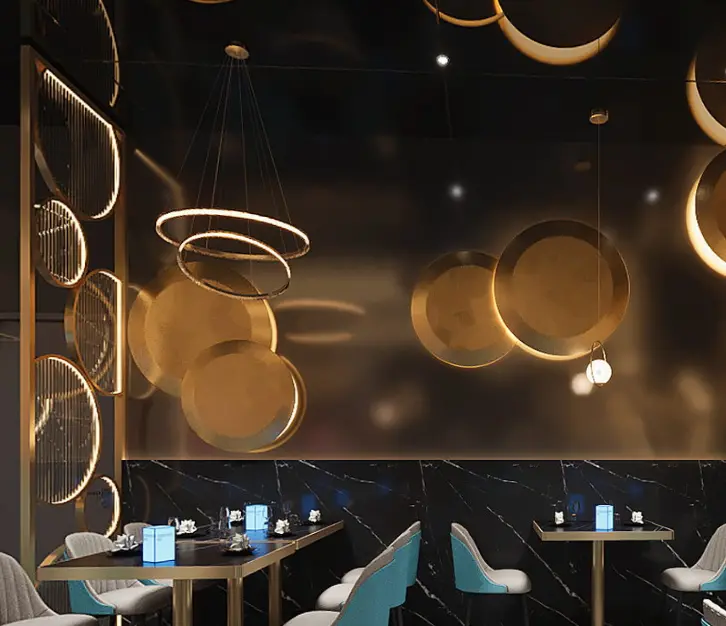
Design referenceCircular wall features shown in the design context
Factory completedCircular stainless-steel wall feature with warm backlighting

Verification

Every assembly checked before sea shipment.

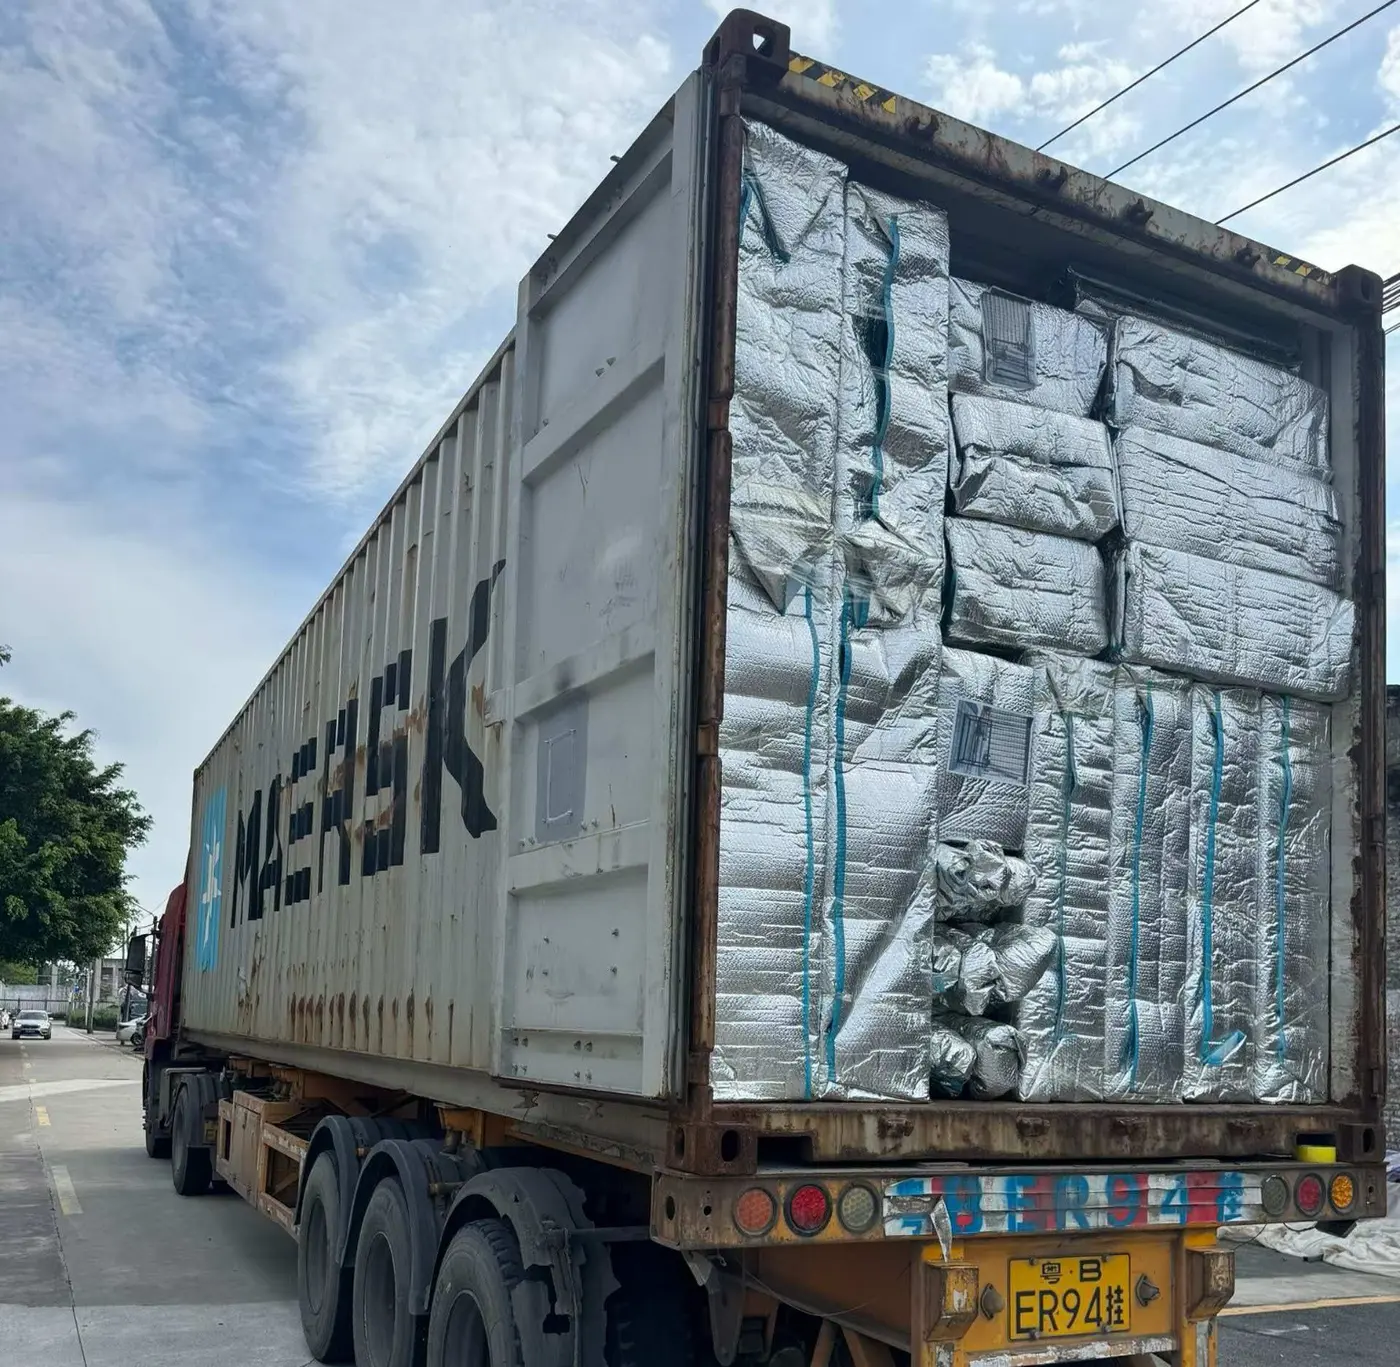
All 72 assemblies were trial fitted, lighting was electrically tested, and separated components were numbered before protective EPE packing.
Overall dimensions
Curve and interface fit
Structural alignment
Surface finish
Glass integration
Lighting function
Component numbering
Packing readiness
40-foot sea containerProtected project components loaded into a 40-foot sea container
Project record: this case documents design input, production, completed assemblies, checks and loading. Installation was completed by the client’s team with FABRITERA remote video guidance. Completed-site photography is not currently available, so no undocumented installation claim is made.
04 / Outcome

August 2023

Seventy-two assemblies.
Dispatched in twenty-six days.

The package was completed, checked and shipped by sea in a 40-foot container without delaying the agreed dispatch date.

The client’s verbal feedback specifically recognised the fidelity between the renderings and the manufactured result.

View all project case studies